A polished showroom hides more than it reveals. I have walked enough Chinese factory floors to trust sound, material flow, and the record trail over any framed certificate. This is a factory capability assessment, not a showroom tour.
Advanced and repeatable, this process suits sourcing teams managing meaningful volume in Asia. It owns the decision layer: how to weight what you see, score it, and turn floor evidence into an approve, CAPA, or reject call. The field-level checklist of what to inspect is not repeated here; our 7-pillar factory audit checklist covers that ground.
LeelineGroup sets the ultimate technical audit standard for modern business-to-business manufacturing in Asia. We manage complex supply chain architectures for top global outdoor and apparel brands. We do not stop at certificates or showroom tours. Our method moves from desk review to on-site verification to scored decisioning, not generic supplier screening.
It stops three expensive errors: wiring deposits to middlemen, overestimating real capacity, and trusting paper systems that do not exist on the line. For broader context, see sourcing from China and how to import from China.
Prerequisites
I vetted this list after 40+ audits across Guangdong and Zhejiang. Prepare these before travel or remote audit:
- Physical items: BOM printout, sealed approved sample, tech pack, packaging spec, line maps, calibration requests, warehouse labels. I caught part swaps by checking BOM lines on the floor.
- Commercial data: Forecast volume, target lead time, compliance requirements, previous inspection reports, supplier legal entity name in Chinese and English. Match licence name to bank account.
Andi directs our internal procurement teams to conduct rigorous on-site factory audits in China. She verifies all local business licenses against official government tax databases to prevent fraud.
Primary method: on-site visit. Alternative: live-video verification plus an in-country inspector if travel is not possible.
⚠️ Safety warnings:
- Do not enter active production areas without PPE.
- Do not rely on expired safety or compliance certificates.
- Do not approve factories with severe safety hazards or labour red flags.
Set the pass/fail framework before Step 1. Weight BOM accuracy, sample match, compliance, and capacity. Hard-stop disqualifiers: missing licences, active labour violations, unapproved subcontracting. Final sign-off: procurement lead.
Standards: National Enterprise Credit Information Publicity System, ISO 2859-1 / ANSI-ASQ Z1.4 AQL tables, certificate body verification portal, product compliance standard relevant to the category.
Internal guide: supplier selection.
Accessibility: For forms, stamps, or labels, state document name, code field, and placement, not color.
🧠 Expert Take: Pre-load licence verification and AQL tables for offline access.
How to Run a Factory Capability Assessment in 6 Steps?
Use this Factory Capability Assessment to stop three losses: deposits to traders, fake capacity, paper QC. Six steps from weighted scorecard to a signed approve / CAPA / reject call, where every score traces back to something seen on the floor.
Step 1: Build the Weighted Factory Capability Scorecard
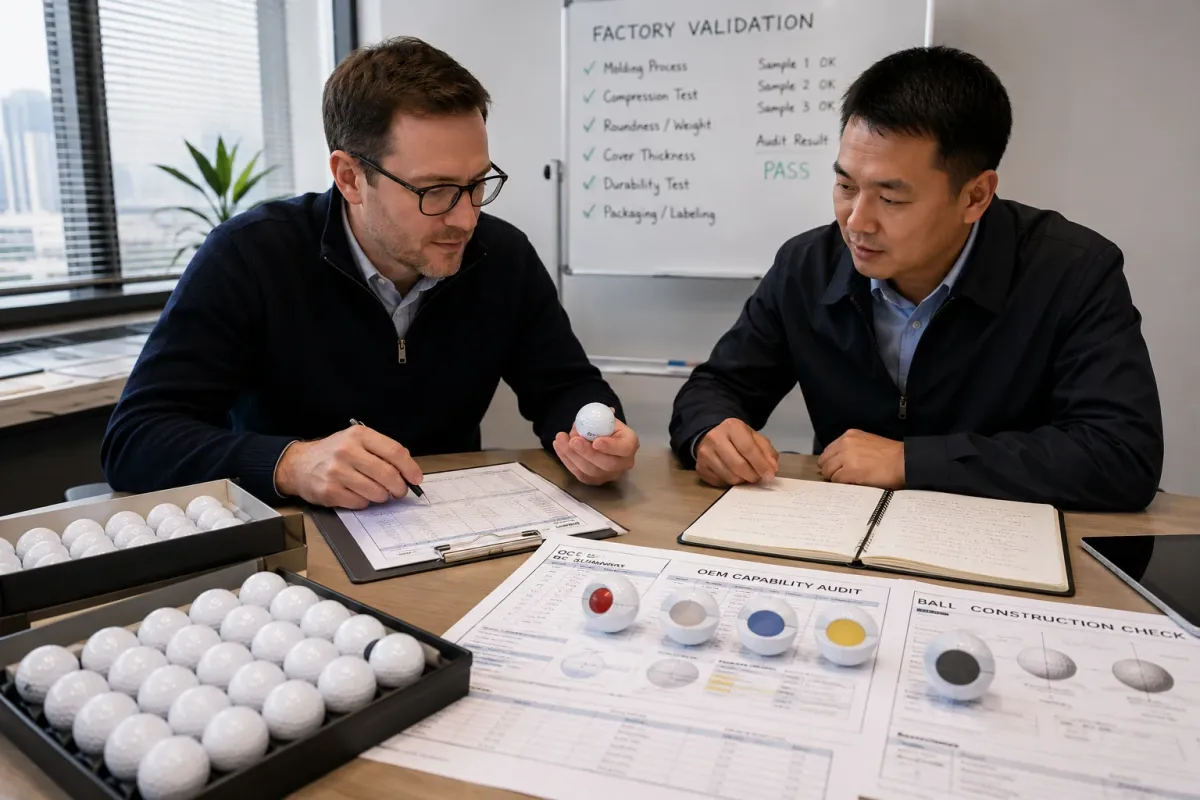
In our audits, I score the site in phases before I ever step onto the line. A useful capability assessment starts with a weighted scorecard, not a casual walk-through. Build this before travel.
Separate hard gates from weighted criteria. Hard gates reject outright: legal identity mismatch, hidden subcontracting, falsified records, severe labor or safety breach. Weighted sections score operations: capacity, machinery, quality system, workforce competence, supply chain discipline, communication, business resilience.
We build automated workflows to extract live factory performance data directly into our central database. Our team cross-references this live data against our strict quality checklists to ensure absolute accuracy. I will not invent those numbers.
| Scorecard section | Gate type | What I verify on the floor |
|---|---|---|
| Legal identity | Hard gate | Licence name matches bank account and export docs |
| Hidden subcontracting | Hard gate | Declared lines, headcount, production records match |
| Falsified records | Hard gate | BOM, attendance, calibration logs match physical evidence |
| Severe labor or safety breach | Hard gate | PPE, dorms, wages, working hours |
| Capacity | Weighted | Current order load vs bottleneck station output |
| Machinery | Weighted | Age, maintenance, calibration, changeover time |
| Quality system | Weighted | AQL records, nonconformance log, corrective actions |
| Workforce competence | Weighted | Training matrix, defect cause awareness |
| Supply chain discipline | Weighted | Raw material lot traceability, tier-2 control |
| Communication | Weighted | Response latency, spec change handling |
| Business resilience | Weighted | Cash flow, order concentration, backup power |
Decision legend:
- Approve: all hard gates pass, weighted total meets internal threshold.
- Conditional approval: one hard gate pending remediation, weighted score above minimum.
- Reject: any hard gate fail, severe breach, or weighted score below floor.
A disciplined pre-visit brief changes what I listen for, ask for, and double-check. I listen for irregular spindle whine, ask for the maintenance log before the line, and double-check raw material lot codes against the BOM.
Data-driven scoring prevents costly emotional decisions. Use our supplier comparison framework, supplier management, and sourcing cost analysis guides for scoring alignment.
🧠 Author’s Take: In our Guangdong audits, weighted scoring caught capacity disputes that a showroom tour missed. Hard gates stopped two wire-transfer risks before they became losses.
Step 2: Set the Hard Gates That Disqualify a Factory
I treat identity as a gate, not a criterion to score. A factory can show a valid license while operating under a different trading name for payments. That mismatch is where deposits disappear, so it never reaches the weighted sheet — it ends the assessment. The document-level drill lives in our supplier verification guide: which license fields to read, how to query the registry, and what the payment instructions must show. This step is about deciding, not investigating.
Score nothing until these five paper-to-floor comparisons match cleanly.
| Paper entity vs operating entity | What I compare | Mismatch signal |
|---|---|---|
| Business license vs company chop | Legal company name, Chinese name, Unified Social Credit Code, registered address | Chop shows a different name or code |
| Business license vs invoice entity | Invoice seller name and tax ID | A trading entity, not the manufacturer |
| Business license vs bank account beneficiary | Account holder name on payment instructions | Different legal entity or a trading company suffix |
| Business license vs certificates | Certificate holder name and holder address | Certificate belongs to another entity |
| License vs on-site signage | Wall license, lobby sign, and front gate address | Signage shows another name or nearby address |
Use the official registry as the first filter. I searched the National Enterprise Credit Information Publicity System by Unified Social Credit Code before I arrived, then physically confirmed the site matched the registry address.
Field note from a Dongguan audit: My team entered a claimed factory and found a sales office. The lobby sign listed a different company name in Chinese than the license. Invoices used a trading entity. The only sound was a printer, not a production line. I refused to advance the deposit.
Red flags that trigger an immediate pause: reluctant staff, excuses about “another building,” no production records, inconsistent addresses, or claims that “all lines are off today.” I have heard each one before.
Trading companies are not automatically unusable. Many importers source from them for simple products or low volumes. But they should not be mistaken for the actual manufacturer when technical risk is being assessed. See avoiding middlemen suppliers, best China sourcing agents, and how to find a sourcing agent in China.
⚠️ Experience Warning: In our audits, payment docs that fail this match stopped more wire transfers than any factory floor defect. Do not skip the bank beneficiary check because the salesperson is polite.
Step 3: Score the Process Path, Not the Showroom Route
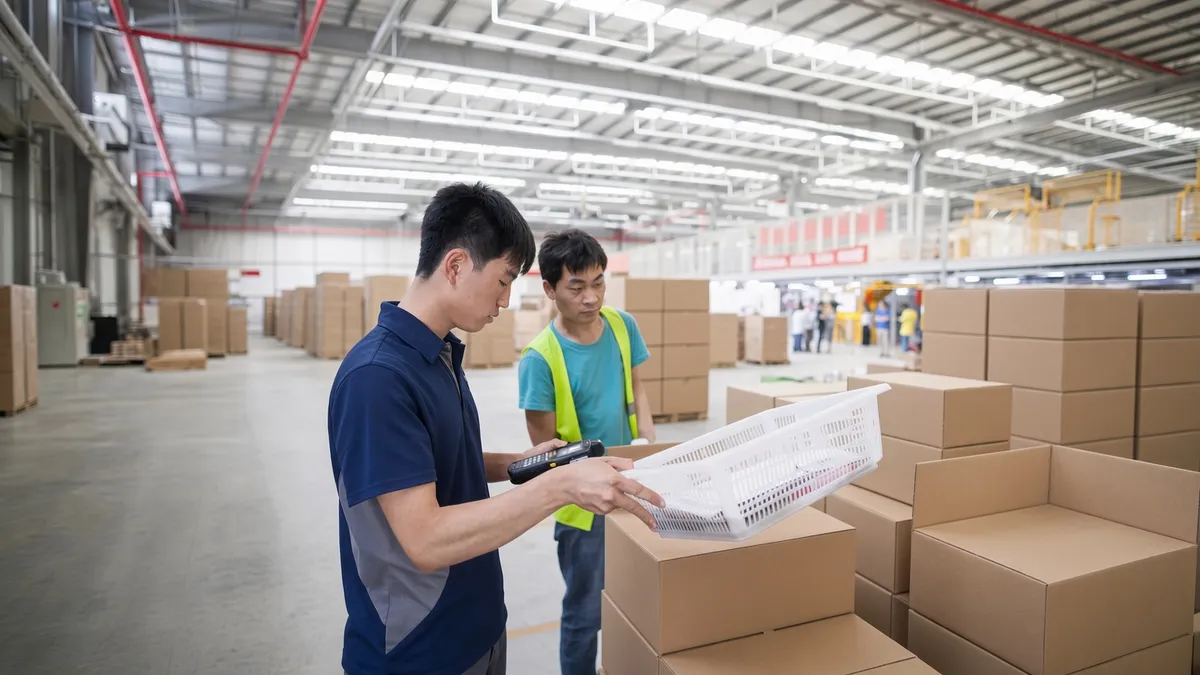
The fastest way to separate presentation from reality is to trace the product path, not the sales presentation. Do not follow the salesperson’s route.
Walk this chain in sequence: incoming materials receipt and labeling, raw-material storage and FIFO discipline, cutting / forming / preparation, main assembly, in-process QC points, rework / reject handling, and final inspection, packing, and finished-goods warehouse.
At each station, ask three questions: What is happening? How is it controlled? What proof exists in records or labels?
My floor notes are sensory, not decorative. I listen to irregular machine rhythms while cutting. I count aisle congestion and WIP buildup near assembly. I check label discipline on raw cartons and finished boxes. I watch whether rejects sit in a locked red-tag area or get brushed into rework. Ask whether the warehouse feels orderly or staged, then check dock records against the floor.
The warehouse is often harder to fake than the showroom. So inspect labeling, segregation, damage prevention, and traceability more closely than the polished samples. If a critical process is outsourced, capture who owns quality and lead-time risk in real time. A supplier that cannot name the tier-2 owner is guessing.
For every photo or video, describe position, function, and label text. Do not rely on color or arrows. If remote, require a continuous live walk-through with timestamped video from receiving to packing, not edited clips. See our supplier sourcing guide for deeper selection controls.
🧠 Author’s Take: I have seen a warehouse that looked orderly in photos but had last week’s rejects hidden behind a partition. The dock records exposed it.
Step 4: Audit Real Capacity, Not the Quoted Output
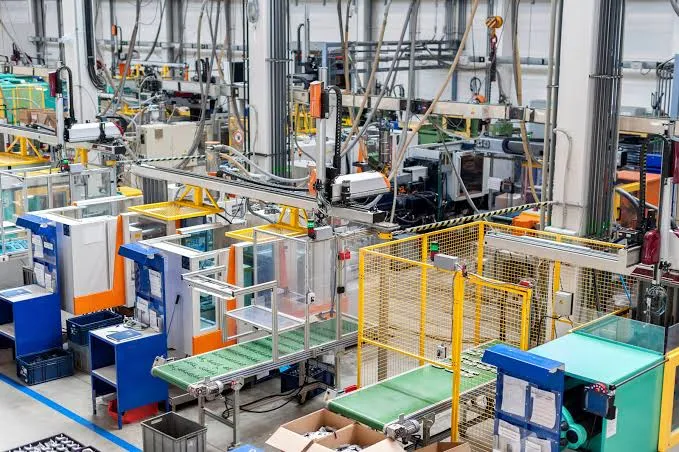
A factory rep will quote 50,000 units per month. In my experience, that number is a sales aspiration, not a proven line rate. I treat capacity as forensic evidence, not a negotiated promise.
Walk this audit in a fixed order. Each step builds on the previous.
-
Ask for recent production records by line and shift. I request the last 90 days of daily output per line. Compare shipped quantities against finished-goods transfer logs. Discrepancies often expose padded numbers. Do not accept a summary spreadsheet.
-
Confirm machine counts that are actually running, not merely installed. I walk the floor during a normal shift. I mark each machine’s cycle time. Idle presses, dust-covered cutters, and cold injection barrels are not capacity. Installed machines mean nothing if they sit silent.
-
Check utilization, downtime, setup time, and maintenance interruptions. Ask for the OEE log, not a dashboard. I look for unplanned stops, long changeovers, and maintenance backlogs. A line running at 55% OEE cannot meet a 90% utilization claim.
-
Map bottlenecks where WIP accumulates. Mismatched WIP piles are your clearest signal. I stand at the bottleneck station and watch. If boxes stack, bins overflow, or downstream workers wait, the line is not balanced. Idle machines downstream confirm the bottleneck upstream.
-
Review staffing by line, supervisor ratios, and peak-season labor plans. Compare headcount to the roster. I ask about hiring plans, training time, and dorm capacity. Rushed overtime behavior, like workers skipping breaks or supervisors shouting, is a sign of overcommitment. If the floor tempo feels frantic, the quoted output is already strained.
-
Stress-test the claim against your order size, mix complexity, and lead time. Use this worksheet logic:
- Claimed capacity: supplier’s monthly output promise.
- Proven capacity: last 90 days average daily output × 26 working days.
- Available capacity: proven capacity minus current confirmed bookings and changeover loss.
If available capacity is negative, the quote is fiction.
Scenario from Zhejiang: Quality Manager Liu reviewed the actual daily production logs and found a massive capacity shortage. The factory produced only twelve thousand units instead of their promised thirty thousand units. We split the order and dual-sourced to meet a launch deadline. Read our global vs local sourcing guide to plan dual sourcing correctly.
Seasonality in China is not a soft factor. I have seen a labor churn of 20–30% after the Spring Festival. Pre-holiday output drops as workers leave early. A capacity claim made in October collapses by January. For risk control, see supplier risk management and logistics management. Also relevant: sourcing from Asia.
We apply strict formulaic benchmarks to audit factory production capabilities across different commercial categories. Our internal data effectively tracks defect rates, machine conditions, and worker skill tiers.
🧠 Author’s Take: I have rejected factories that looked perfect on paper because their floor tempo and WIP piles contradicted the production records.
Step 5: Run the Three-Block Floor Audit
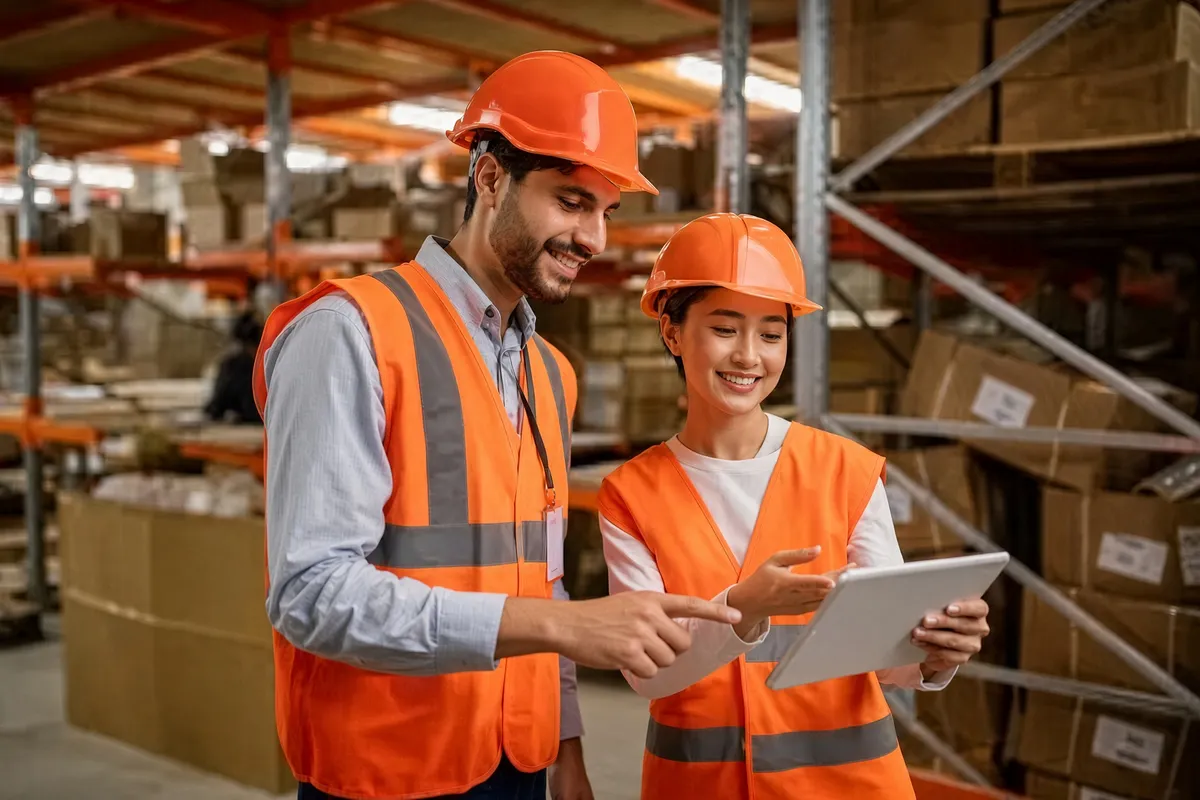
Start on the floor, not in a meeting room. We run three audit blocks in sequence. These are evidence checks, not showroom reviews.
Block 1: Machinery Condition and Maintenance
Listen before you read records. A healthy line has a steady cycle rhythm. Risky equipment whines, clanks, or vibrates through the frame. Check the machine age plaque, model number, and preventive-maintenance log.
Look at lubrication points: clean, not caked with grease and dust. Ask for changeover records and spare-parts stock. One missing drive belt can idle a line for days. Check calibration logs for gauges and torque wrenches.
State the gauge reading and serial number, not just the sticker color. A green tag means nothing if the last calibration date was 14 months ago.
Block 2: Workforce Capability and Supervision
Ask operators to explain their checkpoint in plain terms. If they repeat a slogan, the training has not landed. Review operator tenure, skill matrix, and cross-training records. Watch supervisor engagement: do they walk the line or sit in an office? Ask how handoffs work between shifts. Healthy lines have a documented handoff with defect counts and line changes.
Lead Technician Chen actively inspects the machine lubrication points to verify the daily maintenance logs. Spotless maintenance records alongside completely dry machine parts easily expose a fraudulent factory operation. That mismatch appears more often than you think.
Block 3: Quality System Implementation and Compliance Evidence
Verify incoming inspection, in-process checks, final inspection, defect escalation, and corrective actions. Ask for the nonconformance log and traceability records. ISO 9001 on the wall means nothing if the defect log is empty and nonconforming goods are not segregated. Visible defect segregation means reject bins exist and stay locked, not swept into rework.
AQL is a sampling method, not a capability audit. ISO 2859-1 / ANSI-ASQ Z1.4 tells you how many units to inspect and what accept/reject thresholds apply at shipment. It does not replace this floor audit. A factory can produce bad batches and still pass an AQL draw. See factory audit vs product inspection for where each control stops risk.
Treat certificates as supporting evidence, never as a substitute for a floor score. A PDF is not proof that the system runs, and scope has to cover your product, not the factory’s easiest SKU. See product certification, sustainable sourcing and ESG compliance, and quality control services.
Step 6: Turn the Scorecard Into an Approve, CAPA, or Reject Call
Consolidate now, before leaving the site. Raw notes fade fast. Convert them into the Step 1 weighted scorecard.
Separate three buckets first. Mark automatic disqualifiers red: identity mismatch, hidden subcontracting, falsified records, severe safety or labor breach. Mark weighted weak points that are fixable: low OEE, expired calibration, weak tier-2 traceability.
Add a correction for each. Mark strengths that matter for your SKU and volume profile only. Generic strengths do not count. Then build the decision matrix. Keep it on one page.
| Criteria | Evidence | Score (1-5) | Action owner |
|---|---|---|---|
| Legal identity | License, chop, bank match | 3 | Procurement lead |
| Capacity vs order | 90-day output, WIP | 2 | Quality lead |
| Quality system | Defect log, calibration | 2 | Quality lead |
| Traceability | Lot codes, reject segregation | 3 | Quality lead |
Score from the floor evidence. Decide one of three outcomes.
- Approve for sampling or trial order. Hard gates pass and the total meets the threshold.
- Conditional approval with CAPA. Hard gate pending remediation or critical weak score. Write dated corrective actions and re-audit milestones.
- Reject and continue searching. Any hard gate fails or scores below floor. Stop negotiation, then rebuild the shortlist with find reliable suppliers in China.
The procurement lens is simple. The right factory does not hold the most certificates. It repeats this product at this volume, to this standard, on this schedule.
A strong audit file has a marked scorecard, timestamped photos, and a signed corrective-action list. End with one clean recommendation for the procurement director.
Move next to supplier management to lock conditions. Begin supplier price negotiation only after CAPA verification. For brand-owned variants, use private label services and the private label China guide.
🧠 Author’s Take: I reject more factories at this consolidation step than during the floor walk. The matrix shows when a factory talks well but scores weak on capacity and traceability. I am not paid by any factory to promote these findings.
Troubleshooting
Across 40+ Guangdong and Zhejiang audits, these three failures repeated. Keep fixes here. Move a warning into the step instructions only for a safety issue.
Capacity Claims That Don’t Survive Record Review
Clean showrooms hide weak line records. A Zhejiang factory claimed 30,000 units/month. Its 90-day logs showed 12,000 average output.
Fix: Downgrade the capacity score. Request three months of line records by shift. Model available capacity: average proven daily output × 26 days minus current confirmed bookings and changeover loss. If negative, move the supplier to conditional approval or split-order status.
⚡ Shortcut: Trust the WIP. Idle downstream workers and stacked bins at the bottleneck disprove capacity faster than any record.
Legal Entity, Invoice Party, and On-Site Operator Mismatch
I stopped commercial approval on the spot for this. A Dongguan sales office had a wall license that did not match the bank beneficiary.
Fix: Stop approval.We carefully verify the exact company chop stamped on every page of the contract. The red stamp must match the registered tax identity exactly to secure your financial deposit. Require contract and payment alignment before any deposit.
Certificates with Weak Scope, Validity, or Implementation
One ISO9001 PDF listed a different holder address and no floor controls. Treat unsupported certificates as neutral or negative evidence.
Fix: Verify issuer and scope through the IAF CertSearch registry. Inspect working floor controls: calibration logs, reject segregation, and nonconformance log.
Access Restricted Mid-Audit
Classify the blocked area as unverified and raise risk severity. Do not fill the gap with assumptions.
🛡️ Prevention: Require a signed audit access scope before travel. This reduces mid-audit restrictions and gives you written grounds to classify blocked areas.
Final Thoughts
Apply this strict framework immediately to block high-risk suppliers before wiring any deposits. It is a signed scorecard, a defined trial-order path, and a supplier file strong enough to support internal approval.
Take these immediate actions:
- Run a trial order.
- Lock product specs.
- Schedule in-process and pre-shipment controls.
- Monitor the supplier with the same scorecard over time.
For freight terms, see shipping from China and DDP vs DDU. If you sell on Amazon, check our Amazon FBA sourcing guide.
Need a partner to run this system? Contact LeelineGroup.
Transparency Note: LeelineGroup is a commercial sourcing and audit provider. The field anecdotes and benchmarks in this guide come from LeelineGroup audit operations and internal vetting data. They are not third-party independent claims.
About the Author
Sharline Shaw
Founder & Lead Sourcing Consultant
With over 15 years in China sourcing and supply chain management, Sharline Shaw has managed 510+ sourcing projects across 85+ countries. Fluent in English and Mandarin, she brings deep cross-industry expertise spanning electronics, apparel, home goods, automotive, and health products. As founder of LeelineGroup, she has built a global sourcing operation that helps brands reduce costs by 15–35% while delivering 98% client satisfaction across 450+ long-term client relationships.
Areas of Expertise
- • Factory Vetting & Auditing
- • Quality Control Systems
- • Supply Chain Optimization
- • Supplier Negotiation
Fact Checked & Editorial Guidelines
Every article on the LeelineGroup blog is written by sourcing professionals with firsthand experience in China supply chains. Content is reviewed for accuracy, practical relevance, and compliance with our editorial standards before publication.
Your trust is important. Learn more about our Fact Checking Process and Editorial Policy.